INDUSTRY TRENDS

Plain Cashew Butter Supply Chain: How It’s Made, Where Costs Accumulate, and What QA/Compliance Procurement Should Control

Author
Team Tridge
DATE
August 7, 2026
7 min read
plain-cashew-butter Cover
Unlock Full Data
Plain Cashew Butter Market Intelligence
Prices · Trends · Origins · Forecasts

Plain cashew butter looks like a simple ingredient, but its cost and risk profile is “built in” upstream—through raw nut moisture discipline, kernel yield economics, and low-water-activity food safety controls. This guide maps the real physical flow and shows where procurement (Quality/Safety/Compliance) can set specifications and verification controls that reduce escapes, improve audit readiness, and protect total cost of ownership.

Executive Summary

  • Cost locks in early: Raw cashew nuts are typically dried to ~8–10% moisture after harvest; weak drying/storage increases mold pressure and downstream losses. [1]
  • Kernel conversion is the structural cost center: Shelling/peeling/grading is labor- and yield-driven; this is where breakage and grade recovery set kernel cost. [1]
  • Low-aw doesn’t mean low-risk: Nut butters don’t support pathogen growth well, but Salmonella can survive; safety depends on validated lethality and post-lethality contamination control. [2]
  • Shelf-life is packaging + heat history: Oxygen/light/temperature exposure drives oxidation and sensory drift; logistics can “create defects” without any microbial growth. [3]
  • (Aug 2026 market lens): 2026 crop quality signals (lower outturn/defects) and RCN flow constraints in parts of West Africa are reinforcing premiums for consistent kernels—making spec discipline and alternates more valuable than chasing unit price. [4]

1) The Ground-Truth Physical Map (and the “fixed” cost-drivers)

Plain cashew butter is physically built on the global cashew kernel trade: raw cashew nuts in shell (RCN) are harvested and dried at origin, kernels are produced through labor- and yield-sensitive primary processing, then kernels are roasted and milled into a low-water-activity paste that is microbiologically stable but highly sensitive to post-lethality contamination and oxidation.

Insight: The chain’s cost is “locked in” early by RCN quality (outturn/yield potential) and then compounded by labor-intensive shelling/peeling and grade recovery before you ever grind a single kernel into butter. (Processing flow and typical drying targets are consistent across industry references.) [1]

Data: Industry processing flows consistently show drying → conditioning (often steam/roast) → shelling → drying/peeling → grading → packing as the value-creation sequence; after harvest, RCN are commonly sun-dried to around 8–10% moisture for storage stability. [1]

Procurement Impact: The “physical map” tells you where variance originates: upstream moisture and mold pressure affect mycotoxin risk; primary processing yield/breakage affects kernel cost; roasting/milling and packaging determine safety (post-lethality control) and shelf-life (oxidation) performance.
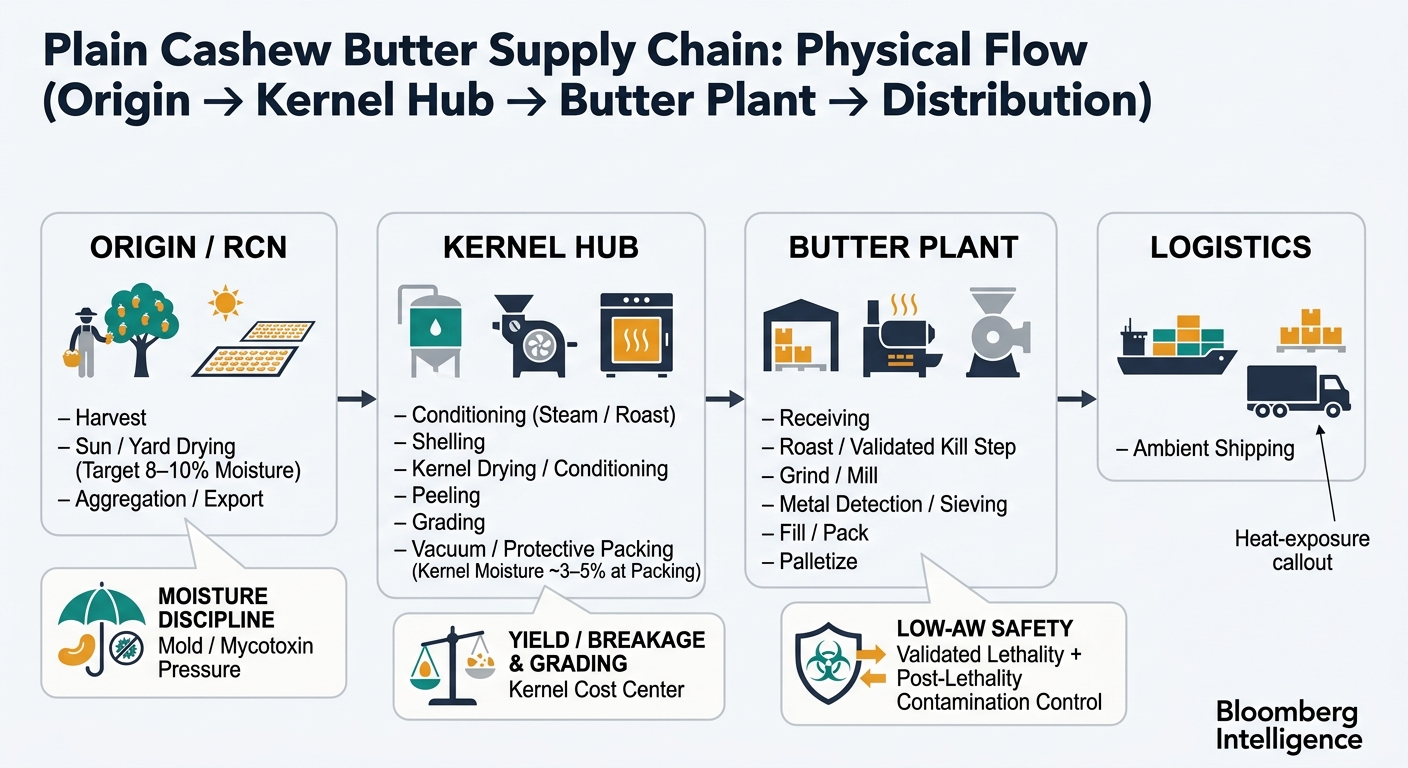
Supply chain flow (simplified)

  • Origin: RCN harvest → sun/yard drying → aggregation/export
  • Kernel hub: conditioning (steam/roast) → shelling → kernel drying/conditioning → peeling → grading → vacuum / protective-atmosphere packing of kernels
  • Butter plant: kernel receiving → roast/kill step → grind/mill → metal detection/sieving → fill/pack → palletize/ship
A left-to-right (or top-to-bottom) flow diagram showing the end-to-end physical chain with 4 grouped blocks and key sub-steps inside each block: (1) Origin/RCN: harvest → sun/yard drying (target 8–10% moisture) → aggregation/export; (2) Kernel hub: conditioning (steam/roast) → shelling → kernel drying/conditioning → peeling → grading → vacuum/protective packing (kernel moisture ~3–5% at packing); (3) Butter plant: receiving → roast/validated kill step → grind/mill → metal detection/sieving → fill/pack → palletize; (4) Logistics: ambient shipping with heat-exposure callout. Includes callouts/icons for the three fixed cost/risk drivers: moisture discipline (mold/mycotoxin pressure), yield/breakage & grading (kernel cost center), and low-aw safety (validated lethality + post-lethality contamination control).

2) Where Cost and Margin Physically Build Up (node-by-node)

Insight: Plain cashew butter has fewer “transformations” than many foods, but each transformation is expensive because it is either (a) yield-destructive (breakage, rejects) or (b) control-intensive (food safety, foreign material, oxidation control).
1. Upstream / Raw Material (RCN farming, drying, aggregation)

  • Insight: The first structural cost driver is not “farming inputs”—it’s post-harvest drying discipline and quality sorting at origin, because moisture and damage determine storage stability, mold pressure, and downstream yield.
  • Data: RCN are commonly dried to roughly 8–10% moisture after harvest to stabilize for storage/transport; poor drying/storage is widely recognized as a driver of quality deterioration and mold risk. [1]
  • Procurement Impact: Even though your purchase is “butter,” the physical cost stack starts here: higher defect/mold pressure upstream becomes higher testing/segregation losses later, and it also increases the probability of shipment holds in strict markets.

2. Primary Processing (RCN → edible kernels)

  • Insight: This is the chain’s most structurally expensive conversion because it is labor-intensive and yield-sensitive: shelling/peeling creates breakage (grade loss), and grading determines how much value you recover.
  • Data: Industry bodies describe the canonical steps as conditioning/roasting → shelling → drying → peeling → grading → QC/packaging; export/packing references commonly manage kernel moisture into a narrow band (often ~3–5%) to support stable packing and reduce breakage or spoilage risk. [1]
  • Procurement Impact: Kernel cost is the dominant input into butter. Physically, you are buying (1) recovered kernel mass and (2) recovered kernel quality. Any upstream or processing-driven breakage/reject rate is a direct cost amplifier before manufacturing overhead is added.

3. Secondary Processing (kernels → plain cashew butter)

  • Insight: Butter manufacturing looks simple (roast + grind), but the fixed cost drivers are food-safety validation at low water activity and foreign-material controls in a sticky, high-fat matrix.
  • Data: FDA notes nut butters and spreads have been associated with Salmonella outbreaks, and FDA guidance highlights that Salmonella can be more heat resistant in low water activity foods (which is why validated lethality plus prevention of recontamination matters). [2]
  • Procurement Impact: The physical “kill step + hygienic zoning” is where safety is made or lost. If the plant’s post-roast environment and equipment design are not robust, the product’s low aw becomes a liability (survival without growth) rather than a safety advantage.

4. Packaging & QA (oxygen/light barrier + traceability + verification)

  • Insight: Packaging is a shelf-life control system: oxygen ingress, light exposure, and headspace management influence oxidation (rancidity) and sensory drift—especially for “plain” formulas without strong masking flavors.
  • Data: Storage research on cashews links oxidation markers (e.g., peroxide value) and storage conditions to quality deterioration and off-flavor development; this supports treating barrier and storage/handling as part of the technical system, not a “marketing” choice. [3]
  • Procurement Impact: Packaging specs (barrier performance, closures, liners for bulk) are not cosmetic—they are part of the technical spec. Weak packaging shifts cost into complaints, returns, and rework even when the butter was manufactured correctly.

5. Logistics & Distribution (ambient, heat exposure, handling)

  • Insight: Cashew butter ships ambient, but heat abuse is a real physical cost driver because it accelerates oxidation and increases oil separation—creating “quality defects” without any microbial growth.
  • Data: Nut quality references consistently show storage temperature and time accelerate oxidative deterioration; the practical takeaway is that thermal excursions are a controllable variable (lane choice, dwell time, container management), not just a freight cost line. [3]
  • Procurement Impact: Distribution conditions determine whether you receive product that behaves like your bench sample. Heat management is part of the physical spec (and part of the cost stack), even if no cold chain is used.

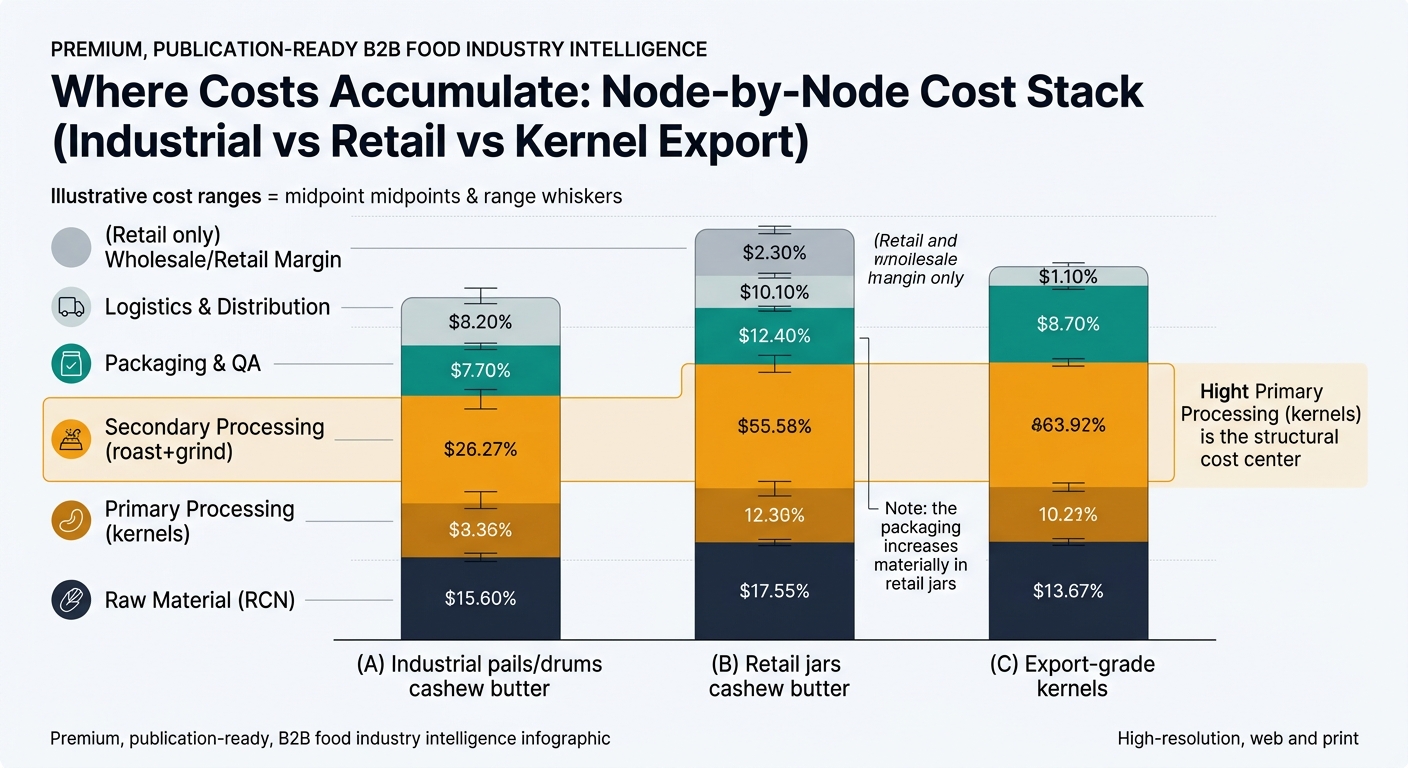
Product-Level Cost Breakdown (illustrative ratios anchored to physical cost drivers)

A stacked bar chart with three bars labeled: (A) Industrial pails/drums cashew butter, (B) Retail jars cashew butter, (C) Export-grade kernels. Each bar is segmented by the same nodes: Raw Material (RCN), Primary Processing (kernels), Secondary Processing (roast+grind), Packaging & QA, Logistics & Distribution, and (Retail only) Wholesale/Retail Margin. Uses the article’s illustrative percentage ranges by showing midpoints (or range whiskers) for each segment, with an emphasis annotation that Primary Processing (kernels) is the structural cost center and a note that packaging share increases materially in retail jars.

A) Plain Cashew Butter (industrial pails/drums)

Supply Chain Node Cost Ratio (% of Final Cost) Notes
Raw Material (RCN at origin) 20–30% Farmgate + aggregation + drying losses; quality determines mold/mycotoxin pressure.
Primary Processing (kernels) 35–45% Labor + yield recovery + grading; kernel cost becomes the dominant input into butter. [1]
Secondary Processing (roast + grind) 10–15% Energy + throughput + validated lethality + hygienic zoning controls. [5]
Packaging & QA 8–12% Liners, pails/drums, coding/traceability, micro/chem verification, metal detection.
Logistics & Distribution 5–10% Inland + ocean + warehousing; heat exposure risk can convert to quality losses.

B) Plain Cashew Butter (retail jars)

Supply Chain Node Cost Ratio (% of Final Cost) Notes
Raw Material (RCN at origin) 12–20% Same upstream physics; diluted by downstream packaging and channel margin.
Primary Processing (kernels) 25–35% Kernel conversion remains the biggest “food” cost component.
Secondary Processing (roast + grind) 8–12% Process controls + line sanitation for allergen environment.
Packaging & QA 15–25% Jar/lid/label/case pack; barrier performance influences oxidation and returns.
Logistics & Distribution 8–12% More touchpoints, more handling damage risk.
Wholesale/Retail Margin 10–20% Channel structure; not a manufacturing cost but part of final shelf cost.

C) Export-Grade Cashew Kernels (vacuum packed cartons)

Supply Chain Node Cost Ratio (% of Final Cost) Notes
Raw Material (RCN) 30–40% Outturn/yield potential is set here; moisture control is foundational. [1]
Primary Processing 45–55% Shelling/peeling/grading labor + breakage losses; value recovered via grade. [1]
Packaging & QA 5–10% Vacuum/protective atmosphere, moisture control (often ~3–5% at packing), metal detection/QC. [6]
Logistics 5–10% Ocean freight + warehousing; moisture/heat excursions degrade quality.
Unlock Full Data
Plain Cashew Butter Market Intelligence
Prices · Trends · Origins · Forecasts

3) Structural Facts You Can’t “Engineer Away” (plan your specs around them)

Insight: Three structural realities govern quality and cost in plain cashew butter: upstream mold pressure, primary-processing yield economics, and low-moisture pathogen survival dynamics.

1) RCN moisture discipline is the first gate for mycotoxin and quality stability

  • Insight: If drying/storage is weak, you inherit a higher probability of mold pressure and quality degradation.
  • Data: Multiple industry references describe drying RCN to around 8–10% moisture for stability; this is a foundational control point for storage and transport. [1]
  • Procurement Impact: Specs and verification should treat upstream moisture/defects as a root-cause variable, not just a receiving defect.

2) Kernel processing is structurally labor- and yield-driven (and grading is the value lever)

  • Insight: The kernel hub is where margin is made or lost through breakage control and grade recovery.
  • Data: Standard processing sequences consistently emphasize shelling/peeling/grading, and export handling commonly conditions kernels to a controlled moisture band for packing performance and stability. [1]
  • Procurement Impact: Even for “plain butter,” kernel grade mix and defect thresholds show up as flavor variance, color variance, and oxidation propensity.

3) Low-moisture foods don’t let pathogens grow—but they let them survive

  • Insight: Safety hinges on validated lethality and prevention of recontamination after the kill step.
  • Data: FDA guidance and outbreak history emphasize nut butters as a relevant vehicle and highlight increased heat resistance of Salmonella in low water activity foods, reinforcing the need for validated controls and hygienic separation. [5]
  • Procurement Impact: Your technical spec should explicitly distinguish “lethality achieved” from “post-lethality protected,” because the physics of low aw changes the failure mode.

Key Insights (what to remember when you read a spec or COA)

  • Kernel conversion is the cost center: Primary processing (shelling/peeling/grading) is the structurally expensive step that dominates the food cost component. [1]
  • Moisture is upstream leverage: RCN moisture discipline (~8–10% at origin) is a physical prerequisite for stable storage and lower mold pressure. [1]
  • Safety is about recontamination control: Low aw reduces growth, not survival; validated roasting plus hygienic separation is the practical control logic. [5]
  • Shelf-life is packaging + thermal history: Oxidation and sensory drift move with storage conditions; packaging barrier and heat exposure are quality variables. [3]

4) The Bottom Line for Your Next Contract

(Analyzed at: Aug, 2026) The 2026 cashew market is rewarding consistency: crop-quality commentary points to weaker outturns and higher defects in several origins, which tightens availability of “clean, predictable” kernels and raises the hidden cost of variability. [4]

Write your next plain-cashew-butter contract so it hard-codes three non-negotiables: (1) upstream moisture/defect expectations (to reduce mold/hold risk), (2) a validated lethality step plus explicit post-lethality controls (to prevent low-aw Salmonella surprises), and (3) packaging + lane requirements that limit oxygen and heat exposure (to protect shelf-life).

This works because it aligns your spec to the chain’s fixed cost nodes—yield recovery, post-roast hygiene, and oxidation control—and can easily be the difference between “normal” receiving and a six-figure year of extra testing, holds, rework, and customer complaints when the market tightens.
Unlock Full Data
Plain Cashew Butter Market Intelligence
Prices · Trends · Origins · Forecasts

References

  1. cashews.org
  2. fda.gov (Salmonella)
  3. agriculture.institute
  4. shop.ofi.com
  5. fda.gov (Guidance for Industry: Salmonella in foods containing peanut)
  6. manage.gov.in

Related Contents

Subscribe
By subscribing you agree to with our Privacy Policy and provide consent to receive updates from our company.
Thank you! Your submission has been received!
Oops! Something went wrong while submitting the form.
Subscribe to receive the latest blog posts, updates, promotions, and announcements from Tridge.