INDUSTRY TRENDS

How Salted Cashew Butter Really Moves (and Where QSC Cost & Risk Lock In)

Author
Team Tridge
DATE
August 7, 2026
8 min read
salted-cashew-butter Cover
Unlock Full Data
Salted Cashew Butter Market Intelligence
Prices · Trends · Origins · Forecasts

Salted cashew butter looks like a simple “jarred ingredient,” but your real exposure is upstream: kernel yield economics, low‑moisture pathogen controls, oxidation management, and heat during distribution. This guide maps the physical chain the way Quality/Safety/Compliance (QSC) teams need it—so you can tie specs, documentation, and change control to the exact nodes where cost and risk become hard to reverse.

Executive Summary

  • Chain reality: Cashew butter is inherently multi‑node (RCN → kernels → roast/grind → pack → distribute), which is why documentation gaps and spec drift are common.
  • QSC risk focus: Low‑moisture foods (including nut butters) still require validated lethality and strong sanitation/EMP discipline to manage Salmonella risk. [1]
  • Quality lever: Packaging barrier + seal integrity often explain rancidity/separation complaints better than “formula tweaks.”
  • Cost lock‑in: The biggest structural cost drivers sit at kernel yield/grade strategy and at manufacturing controls (roast validation, EMP, oxidation/temperature control).
  • 2026 market note: Kernel availability/quality tightness has been a recurring 2026 theme in market commentary—making pre‑qualification of alternates and tighter spec governance more valuable than in oversupply years. [2]

1) The Physical Map You’re Actually Buying Into (From Orchard to Jar)

Salted cashew butter is not a “single-origin ingredient” story—it’s a multi-step chain where raw cashews are grown in one set of countries, shelled/graded in another, and roasted/ground/packed somewhere else entirely. That split is the ground truth behind most quality variability, documentation gaps, and lead-time noise.

Insight: The biggest fixed cost-drivers are set before butter exists—at kernel yield (shelling/grading) and at manufacturing controls (validated roast/EMP, oxidation management, packaging barrier).

Data: Typical flow is (1) raw cashew nuts (in-shell) aggregated and exported, (2) industrial shelling/peeling/drying into kernels, (3) roasting + grinding into paste/butter with salt addition, (4) packaging into retail jars or bulk formats, then (5) ambient distribution where heat exposure accelerates rancidity and separation.

Procurement Impact: If you only map “supplier → finished jar,” you miss where the chain locks in cost and risk: kernel yield economics, kill-step validation, and packaging/transport conditions that determine shelf-life outcomes.

  • Quick Win: Draw your internal “bill of process” as five physical nodes (RCN → kernels → roast/grind → pack → distribute) and attach one spec/COA requirement to each node; it instantly reveals where your current spec pack is silent.
A left-to-right flow diagram with 5 labeled nodes: (1) RCN (in-shell) aggregation/export, (2) Primary processing into kernels (conditioning/shelling/peeling/drying/grading), (3) Secondary manufacturing (roast as kill step + grinding/emulsification + salt addition), (4) Packaging & QA release (jar/tub/pail, seal integrity, release checks), (5) Logistics & distribution (ambient lanes with heat exposure). Under each node, include 2–3 small callouts tagged 'Cost Lock-In' and 'QSC Risk Lock-In' (e.g., yield/breakage; kill-step validation & EMP; barrier/seal; time-temperature exposure). Use simple icons (nut, factory, thermometer, jar, ship/truck) and avoid any dashboard/software UI elements.

2) Where Cost and Margin Accumulate (Node by Node)

Insight: In salted cashew butter, costs compound in layers: (a) agricultural variability, (b) kernel recovery/yield and labor intensity, (c) food safety and oxidation control in low-moisture manufacturing, and (d) packaging materials and distribution dwell time.

Data: Kernel input is typically the dominant cost driver in finished butter; processing nodes add value through yield recovery, safety controls, and packaging performance (oxygen/light barrier + seal integrity).

Procurement Impact: When a supplier quote looks “high,” the explanation is usually physical: kernel grade mix, yield loss, kill-step/EMP overhead, packaging format, and QA/testing load—not just margin.
1. Upstream / Raw Material (Cashew Cultivation + RCN Aggregation)

  • Insight: The farm/aggregation node sets the variability envelope—moisture control and storage discipline determine mold risk drivers and downstream reject rates.
  • Data: RCN is harvested seasonally, sun-dried, bagged, and aggregated through traders; quality loss often comes from uneven drying, re-wetting, and long storage in humid conditions (conditions that also increase mold/mycotoxin risk drivers). [3]
  • Procurement Impact: Even though you don’t buy “RCN” for butter, this node determines how much testing and sorting cost shows up later (and how stable kernel quality is lot-to-lot).
  • Quick Win: Ask finished-goods suppliers to disclose RCN origin bands and storage duration assumptions (even in ranges); it’s the simplest proxy for upstream variability.

2. Primary Processing (Conditioning, Shelling, Drying, Peeling, Grading → Kernels)

  • Insight: This is the economic engine of the chain: whole-kernel recovery vs. breakage drives processor margins, and broken grades often feed paste/butter supply.
  • Data: Shelling/peeling remain labor- and energy-intensive; yield loss occurs through breakage, scorching, moisture mismanagement, and rework. Kernel moisture is controlled to protect texture and shelf stability downstream; industry specs commonly target low single‑digit moisture for kernels. [4]
  • Procurement Impact: Butter manufacturers using more broken kernels can have a structurally different cost base and different oxidation behavior than those insisting on higher whole-grade inputs.
  • Quick Win: Add one line to your spec pack: “Kernel grade strategy used for butter (whole/broken mix) + target moisture range at receipt.” It explains texture consistency and rancidity sensitivity.

3. Secondary Manufacturing (Roasting as Kill Step + Grinding/Emulsification + Salt Addition)

  • Insight: This node is where food safety and sensory performance are “manufactured”: validated roasting, sanitation programs and environmental monitoring for low‑moisture ready‑to‑eat foods, grind temperature control, and salt distribution all matter. [1]
  • Data:Salmonella can persist in low‑water‑activity foods and may be more heat resistant in matrices like nut butters/pastes; finished-product testing alone is not sufficient to prove process adequacy. [5]
  • Procurement Impact: The same kernel can become two very different risk profiles depending on roast validation discipline, rework practices, and EMP maturity—this is where QSC scrutiny should concentrate.
  • Quick Win: Require three manufacturing control disclosures in your technical packet: kill-step validation summary, EMP scope/frequency, and maximum grind discharge temperature (or equivalent control).

4. Packaging & QA Release (Jar/Tub/Pail + Seals + Finished Testing)

  • Insight: Packaging is not cosmetic—oxygen/light barrier and seal integrity are structural determinants of rancidity rate and complaint risk.
  • Data: Retail jars (glass/PET), lids, and induction seals add meaningful unit cost; bulk pails/drums reduce packaging cost per kg but increase exposure risk if resealed/reworked poorly. Finished QA commonly includes moisture, oxidation indicators (where used), micro release logic, and foreign-material controls.
  • Procurement Impact: If your complaint pattern is “stale/rancid” or “excess separation,” packaging specs (barrier, headspace, seal checks) and release criteria can be the root cause—not formulation.
  • Quick Win: Put packaging performance into the spec: minimum barrier requirement (or packaging material standard) + seal verification method + storage temperature limits.

5. Logistics & Distribution (Ambient, but Heat is the Hidden Accelerator)

  • Insight: Cashew butter is “ambient,” but it is not heat-neutral; temperature excursions accelerate oxidation and can worsen oil separation.
  • Data: Long ocean transits and inland warehousing can expose product to sustained high temperatures; dwell time and container conditions matter more than distance alone. (This aligns with the broader evidence that higher storage temperature/humidity accelerates oxidation markers in cashew/nut matrices.) [6]
  • Procurement Impact: Two identical lots can age differently depending on time/temperature history, driving inconsistent shelf-life performance and customer complaints.
  • Quick Win: Add a simple logistics control: maximum allowable temperature exposure window (or require temperature recording for long-haul lanes) for high-risk seasons/routes.
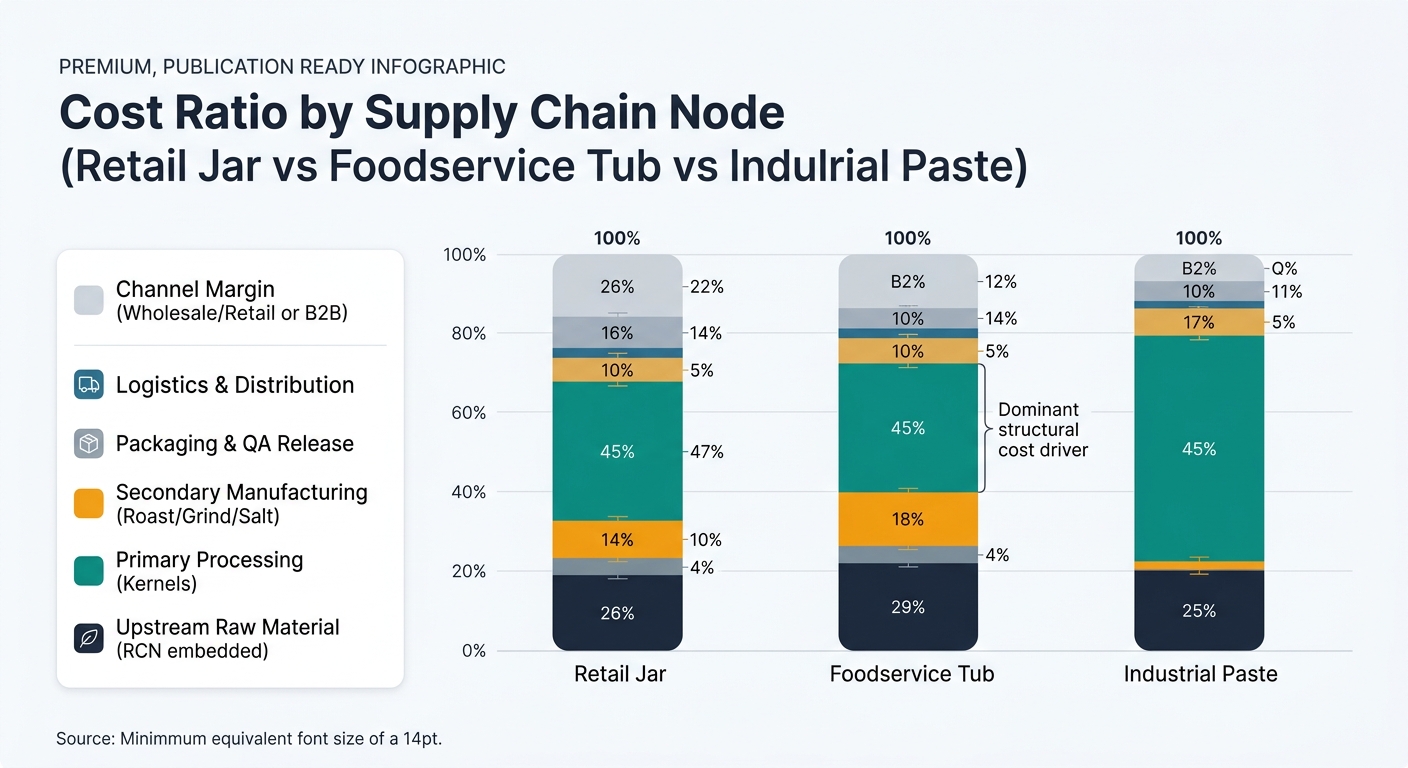
A 3-bar stacked chart (one bar per product format: Retail Jar, Foodservice Tub, Industrial Paste). Each bar is segmented by the same nodes used in the article tables: Upstream Raw Material (RCN embedded), Primary Processing (Kernels), Secondary Manufacturing (Roast/Grind/Salt), Packaging & QA Release, Logistics & Distribution, and Channel Margin (Wholesale/Retail or B2B). Use the midpoint of each stated range to size segments (and optionally add thin whiskers or labels showing the range). Include a legend and annotate the largest segment per format (typically kernels/primary processing) as 'Dominant structural cost driver'.

Product-Level Cost Breakdown

A) Salted Cashew Butter (Retail Jar)

Supply Chain Node Cost Ratio (% of Final Cost) Notes
Upstream Raw Material (RCN embedded in kernels) 10–20% Variability driver; cost realized through kernel price and rejects.
Primary Processing (Kernels: shell/peel/dry/grade) 35–50% Yield recovery + labor intensity; biggest structural value-add before butter.
Secondary Manufacturing (roast/grind/salt) 12–18% Kill-step validation, EMP overhead, energy, throughput, rework.
Packaging & QA Release 12–20% Jar/lid/seal/label + finished release testing and inspections.
Logistics & Distribution 6–12% Heat exposure risk + warehousing time; varies by lane and season.
Wholesale/Retail Margin 10–20% Channel-dependent; not a manufacturing cost but part of final shelf cost.

B) Salted Cashew Butter (Foodservice Tub)

Supply Chain Node Cost Ratio (% of Final Cost) Notes
Upstream Raw Material (RCN embedded in kernels) 10–20% Similar upstream drivers as retail.
Primary Processing (Kernels) 38–55% Still dominant; grade strategy (broken mix) can shift cost.
Secondary Manufacturing (roast/grind/salt) 12–20% Throughput efficiency matters; rework controls are critical.
Packaging & QA Release 6–12% Lower unit packaging cost than jars; sealing still critical.
Logistics & Distribution 6–12% Bulk formats can reduce handling but increase exposure if opened/resealed.
Wholesale/Distributor Margin 8–15% Channel structure differs vs. retail.

C) Industrial Cashew Paste Base (Unsalted or Lightly Salted, Bulk Pail/Drum)

Supply Chain Node Cost Ratio (% of Final Cost) Notes
Upstream Raw Material (RCN embedded in kernels) 10–22% Quality variability shows up as sorting/testing burden.
Primary Processing (Kernels) 45–60% Highest share because packaging/channel margins are lower.
Secondary Manufacturing (roast/grind) 15–25% Paste consistency, grind heat control, foreign-material controls.
Packaging & QA Release 3–8% Lowest packaging share; liner integrity and reseal controls matter.
Logistics & Distribution 5–12% Drums/pails reduce damage but heat exposure still accelerates oxidation.
B2B Margin 5–10% Typically leaner than retail.
Unlock Full Data
Salted Cashew Butter Market Intelligence
Prices · Trends · Origins · Forecasts

3) Structural Realities That Don’t Go Away (Even in “Normal” Markets)

Insight: Salted cashew butter inherits structural constraints from the global cashew kernel system and from low-moisture food safety expectations—these are constants, not trends.

Data: The chain is structurally split across geographies (origin vs. shelling hubs vs. manufacturing/packing), the upstream is seasonal while manufacturing is year-round, and low-moisture foods require disciplined preventive controls (validated lethality + sanitation/EMP) even when water activity is low. [1]

Procurement Impact: Your QSC workload is structurally driven by chain fragmentation: more handoffs mean more documentation edges, more change points, and more ways for spec drift to enter.

  • Reality #1 — Processing concentration is real: A large share of shelling/grading capacity has historically sat in a few processing hubs, while raw nuts are grown across West Africa and parts of Asia. That concentration makes kernel availability and quality more correlated than teams expect.
  • Reality #2 — Seasonality upstream, continuous downstream: Harvest windows create quality and moisture variability that can surface months later as oxidation differences or higher reject rates in kernels/paste.
  • Reality #3 — “Ambient” does not mean “stable”: Heat exposure in transit/warehousing is a structural shelf-life risk driver for high-fat nut products; it silently changes oxidation trajectory and sensory acceptance even without obvious package damage. [6]
  • Quick Win: Treat time/temperature history as a spec attribute (like salt % or particle size), not as a logistics afterthought.

Key Insights You Can Use Immediately (Without Changing Strategy)

  • Key Takeaways: The chain’s biggest cost lock-in happens at kernel yield recovery (shelling/grading) and at manufacturing controls (validated roast + sanitation/EMP + grind heat control).
  • Key Takeaways: Packaging is a structural quality lever; barrier properties and seal integrity often explain rancidity and separation complaints better than formulation tweaks.
  • Key Takeaways: Heat exposure during distribution is the hidden accelerator; “ambient” lanes can still behave like accelerated shelf-life tests in hot seasons.
  • Key Takeaways: Grade strategy (whole vs. broken kernel mix) is a physical driver of both cost and performance; it should be disclosed in technical documentation.

4) The Bottom Line for Your Next Contract

(Analyzed at: Aug, 2026)

In the 2026 cashew market, multiple industry updates have pointed to weaker crop quality and tighter availability of higher‑quality raw inputs—conditions that make kernel variability and supplier change events more likely to show up downstream. [2]

Put one high‑conviction control into your next salted cashew butter agreement: make “process + pack” evidence contractually versioned—(1) kernel grade strategy and incoming moisture target, (2) roast lethality validation plus sanitation/EMP scope, and (3) packaging barrier/seal verification—so any change triggers formal notice and QSC review. This works because those are the three nodes where cost and risk become irreversible; if they drift without visibility, you pay later in holds, extra testing, and shelf‑life complaints that can easily erase a few points of negotiated price improvement.
Unlock Full Data
Salted Cashew Butter Market Intelligence
Prices · Trends · Origins · Forecasts

References

  1. fda.gov
  2. shop.ofi.com
  3. fao.org
  4. afius.org
  5. fda.gov
  6. pmc.ncbi.nlm.nih.gov

Related Contents

Subscribe
By subscribing you agree to with our Privacy Policy and provide consent to receive updates from our company.
Thank you! Your submission has been received!
Oops! Something went wrong while submitting the form.
Subscribe to receive the latest blog posts, updates, promotions, and announcements from Tridge.